
Inspection & Measuring: Your Advantages
Find out what is possible with ZOLLER for tool inspections. Process-related inspections or high-end analyses through to SKP, roughness and the creation of digital twins.
Learn more
To ensure that tools perform exactly as planned, they must themselves be manufactured with precision. With our universal measuring machines, tools can be measured to the micrometer and checked to ensure they correspond to the requirements.
The measured probe points are assigned by the measuring machines to a specific length measurement system along a specific axis of travel. The measuring software then processes this information and assigns it to specific points within the entire coordinate measuring system.
Based on the coordinates determined in this way, the CMM software then calculates the values for quantities that are not measured directly—such as lengths, angles, distances between two measuring points, and so on.
The measuring points (actual values) determined in the coordinate measuring system (CMS) are finally compared with the values that result from the specifications—such as the tool designs (nominal values). If these do not correspond—that is, if there are measurement deviations, whether due to manufacturing defects or wear and tear—appropriate corrective action can then be taken.
The term “3D measuring machines” is generally used to designate measuring machines that can measure the three-dimensional geometry of a measurement object in a relatively short time—ideally in real time. When using compact line-scan or matrix cameras, some of these inspection machines can even be handheld or at least portable. However, portable CMMs are generally slightly less accurate than conventional inspection machines.
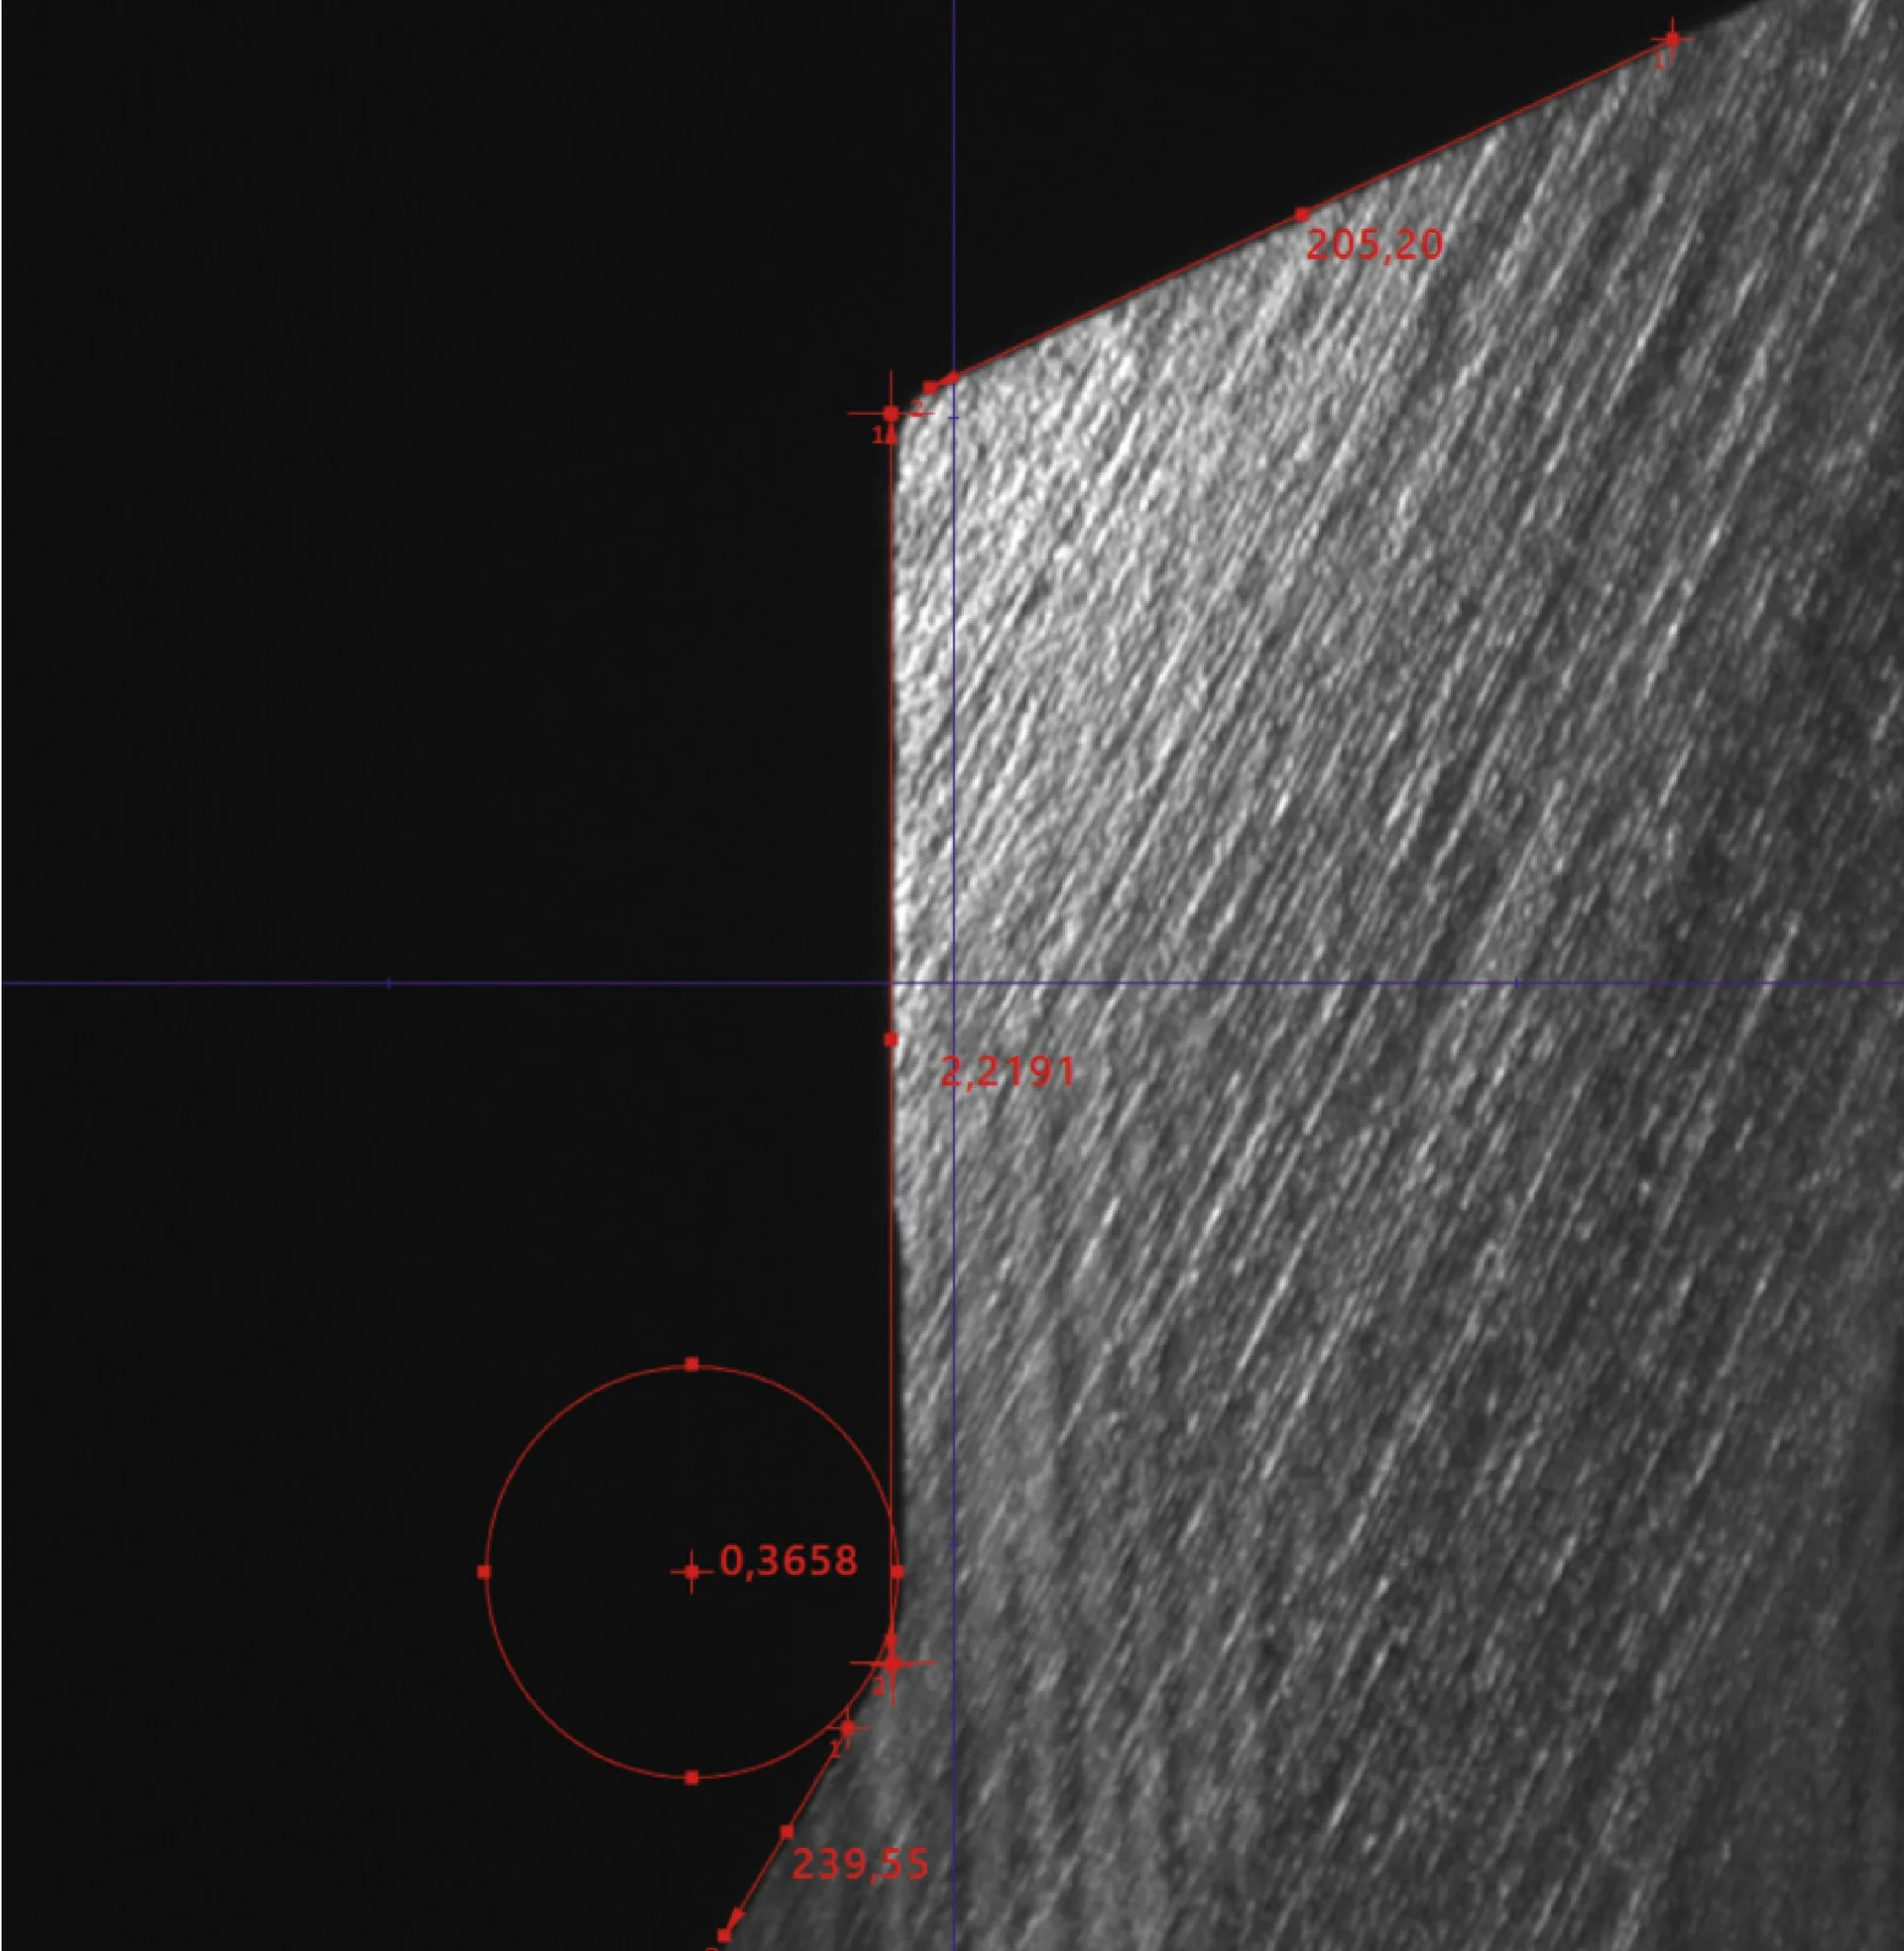
Many measuring machines use what is known as coordinate measuring technology. The measuring machine (the full designation is “coordinate measuring machine,” CMM) uses a suitable sensor to capture the exact coordinates of specific points on the surface of the workpiece.
In most cases, the coordinate system is created parallel to the orthogonal travel axes of the coordinate measuring systems.
Non-contact probing, on the other hand, uses cameras, laser triangulation sensors, and other methods, such as optical or electrical sensors. The measuring process takes place here without a measuring sensor ever coming into contact with the workpiece. Under certain circumstances, this can significantly speed up the measuring process.
For tactile (mechanical) probing of workpieces, measuring sensors or styluses are used; a distinction is usually made between touch-trigger systems (which can only distinguish between the rest state and touch) and measuring systems (which can measure deviations within a narrow area).
Multisensor coordinate measuring machines combine various probing methods not only to achieve especially accurate results but also to provide an especially well-suited measurement method for every requirement.
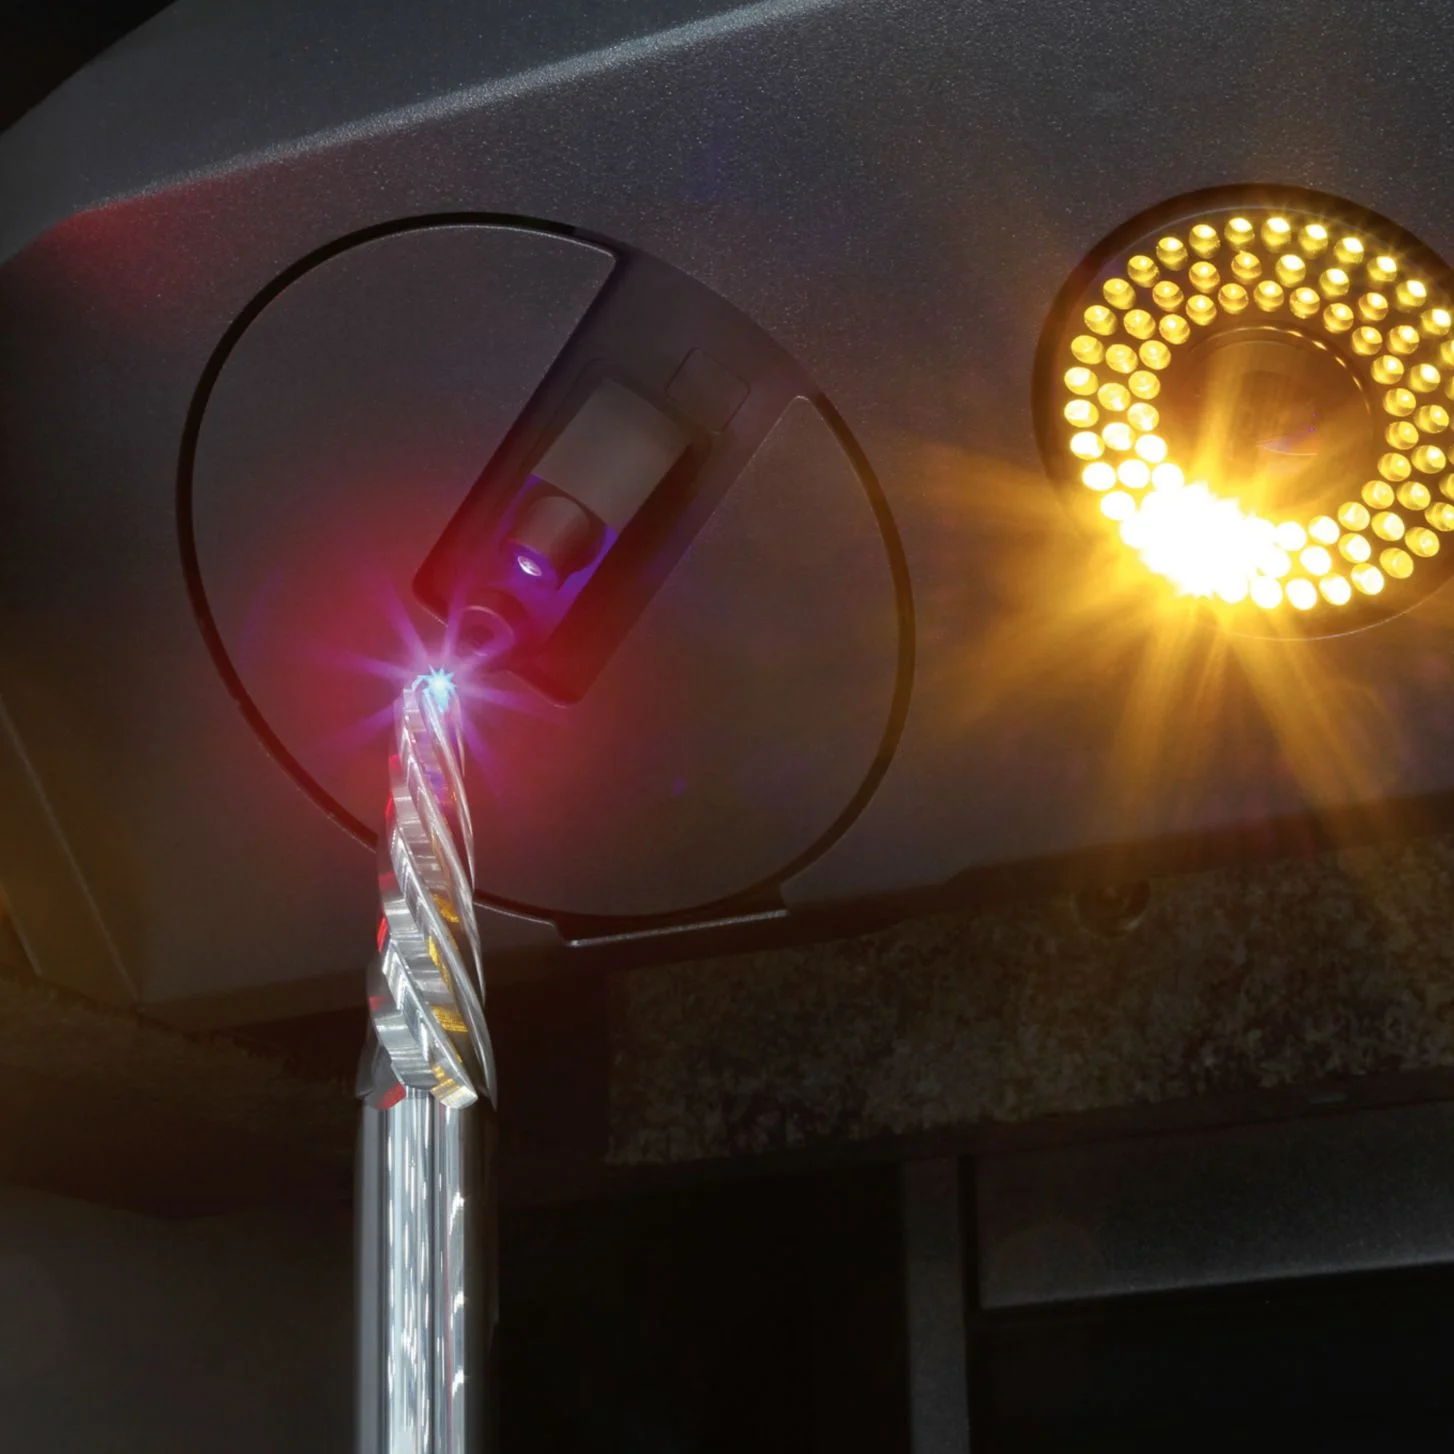
Find out what is possible with ZOLLER for tool inspections. Process-related inspections or high-end analyses through to SKP, roughness and the creation of digital twins.
The individual exchange about your goals and our ideas for achieving them. Online advice from ZOLLER directly from the Smart Factory. Arrange your appointment now.